Food Processing Industry Solution
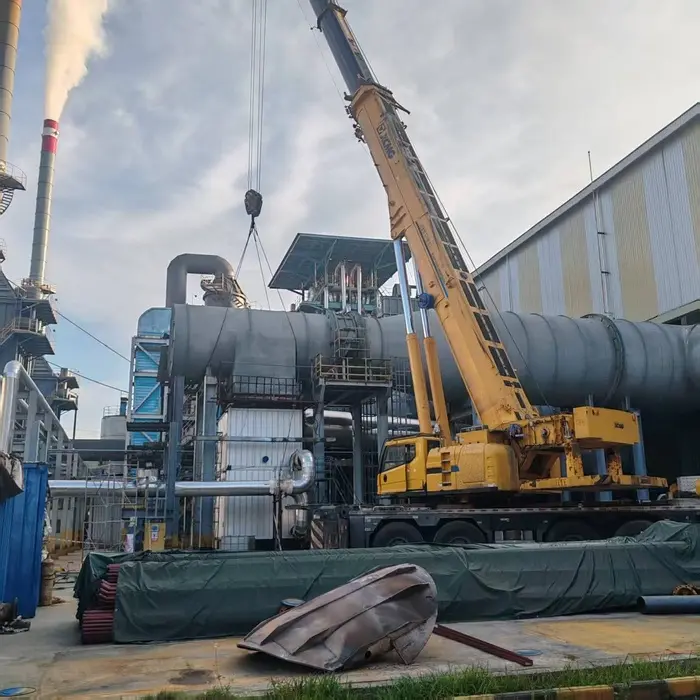
Provide safe and energy‑complete thermal system solutions including thermal oil heaters and waste heat recovery units for heating demands of cooking, drying, sterilization and other processes in food processing, to meet hygienic, stable and compliant production requirements of the food industry.
Solution Overview
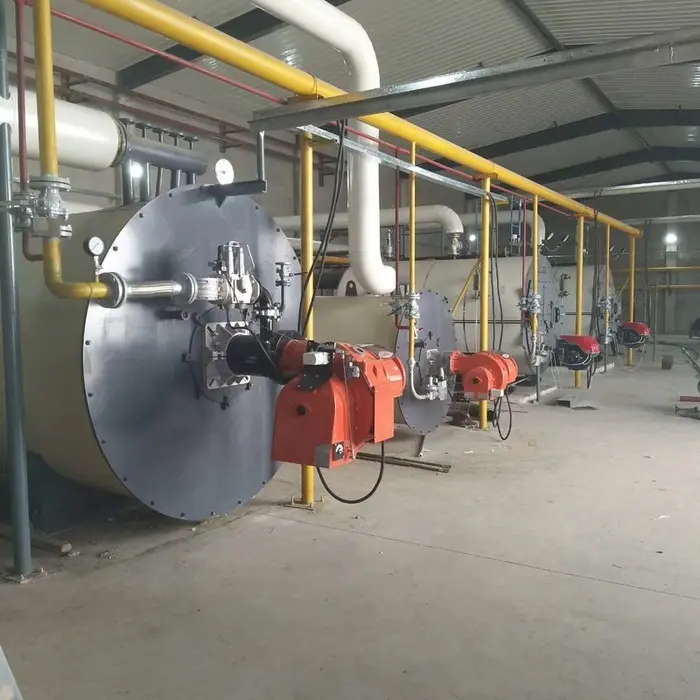
The food processing industry covers numerous sub‑scenarios including baking, meat product processing, grain‑oil processing, fruit‑vegetable drying, can sterilization, and condiment boiling. Continuous and stable high‑temperature heat sources are required throughout production. This solution delivers a full set of industrial thermal equipment, including gas‑fired / biomass thermal oil heaters, waste‑heat recovery systems, heat‑exchange units and temperature‑control supporting systems. It meets strict food‑plant requirements for safety, sanitation, temperature‑control accuracy and environmental emission standards, helping enterprises cut energy consumption and guarantee continuous production.
Applicable Scenarios
Grain‑oil processing: heating for oil refining, oil pressing and deodorization processes
Bakery food: drying and curing heating for biscuit and pastry production lines
Meat product processing: heat supply for cooking, marinating‑boiling and sterilization procedures
Fruit‑vegetable processing: thermal treatment for dried fruit and dehydrated vegetable production
Condiments: sauce boiling, fermentation heat preservation, concentration and evaporation
Cans & beverages: sterilization, preheating and tank heating processes
Technical Route
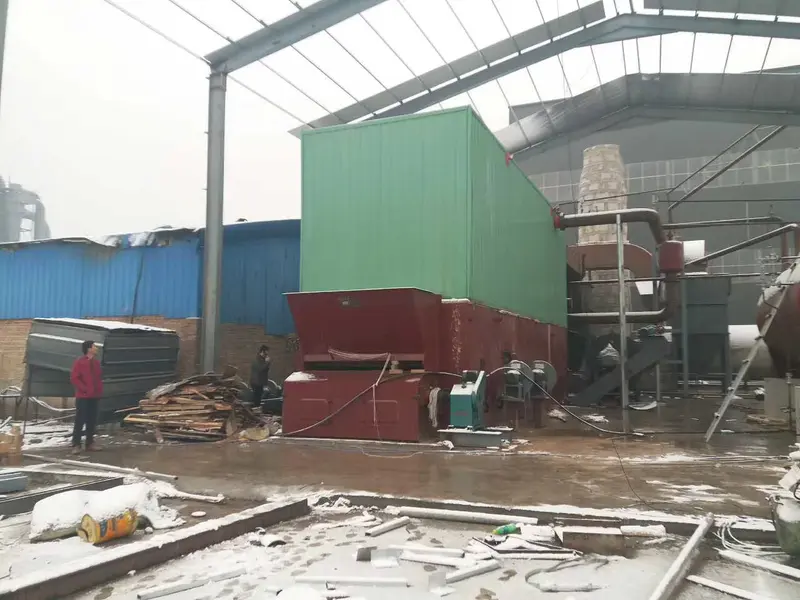
Heat source selection: Gas‑fired thermal oil heaters or biomass boilers are optional according to factory fuel conditions, equipped with waste‑heat recovery devices to recycle flue‑gas waste heat and cut fuel consumption.
Heat exchange & temperature control: High‑efficiency heat exchangers are adopted for indirect heat exchange to avoid medium contamination, with controllable temperature‑control accuracy to satisfy food‑production hygiene standards. Multiple safety interlock protections are configured for automatic alarm and shutdown under over‑temperature, over‑pressure and low liquid‑level conditions.
System integration: Complete circulating pipelines, filter assemblies, expansion tanks and control systems are provided. Connection to factory DCS is supported for remote monitoring and stable non‑stop heat supply 24‑hours a day.
Environmental compliance: Optimized combustion system to meet waste‑gas emission standards and pass local environmental‑protection acceptance. Equipment materials satisfy cleanliness requirements for food‑processing plants.
Solution Values
Stable temperature control: Uniform and adjustable temperature prevents product quality fluctuation and guarantees consistent finished‑product quality.
Energy‑saving & consumption reduction: Waste‑heat recovery effectively cuts fuel costs and improves plant economic benefits.
Safety & reliability: Multi‑layer safety protection reduces production‑accident risks and adapts to non‑stop production mode of food plants.
Customized flexibility: Non‑standard packaged design available according to factory capacity, site space and fuel conditions. One‑stop service including installation and commissioning is provided.
Other Solutions
Heating Solution for Chemical Industry
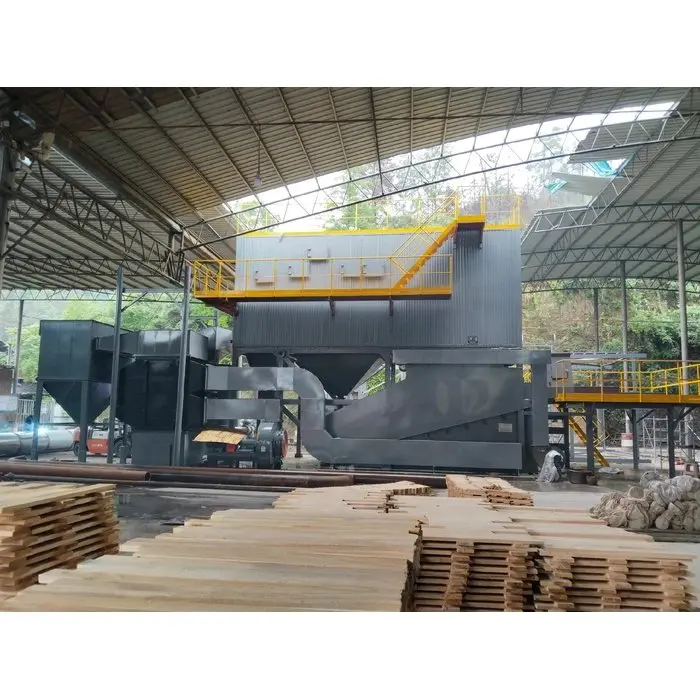
Heating Solution for Chemical Industry Adopts a closed‑loop heating system consisting of "thermal oil heater + high‑temperature circulating pump + heat exchange for heat‑consuming equipment + automatic control". The organic heat‑carrier furnace heats the thermal oil to 280~350℃. Forced circulation by the high‑temperature circulating pump delivers hot oil stably to heat‑consuming equipment such as reaction kettles, distillation columns and evaporators to achieve precise constant‑temperature heating. It features high temperature‑control accuracy, safe and reliable operation under atmospheric pressure, and thermal efficiency ≥90%. Suitable for heating processes in petrochemicals, fine chemicals, printing & dyeing, oil & fat, asphalt and other industries. Customizable according to heat load, fuel conditions and explosion‑proof grades. Full‑range services including design, supply, installation and operation‑maintenance are available.
Textile Dyeing Industry Solution
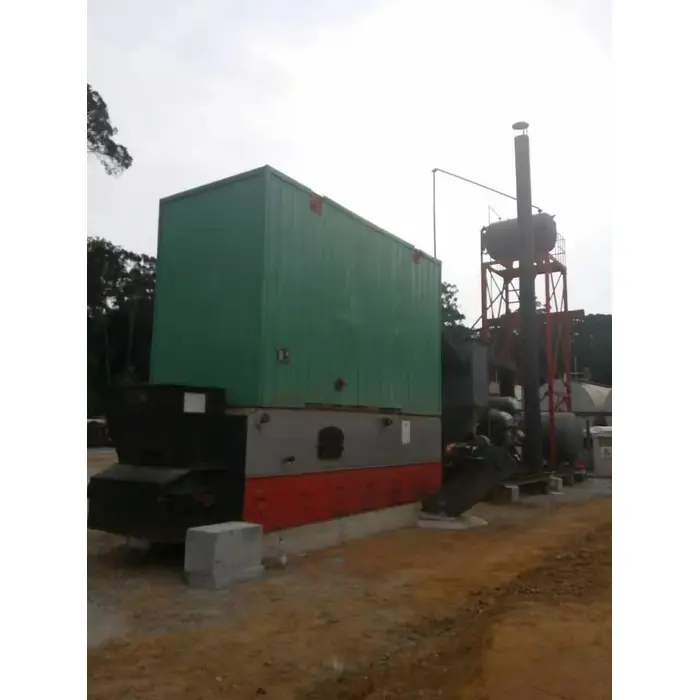
Aiming at the pain points of high energy consumption and high emissions in textile printing and dyeing, we provide an integrated thermal solution of thermal‑oil heater plus waste heat recovery to cut energy consumption in printing and dyeing production, achieving energy‑saving, cost reduction and environmental compliance.
Asphalt Solutions
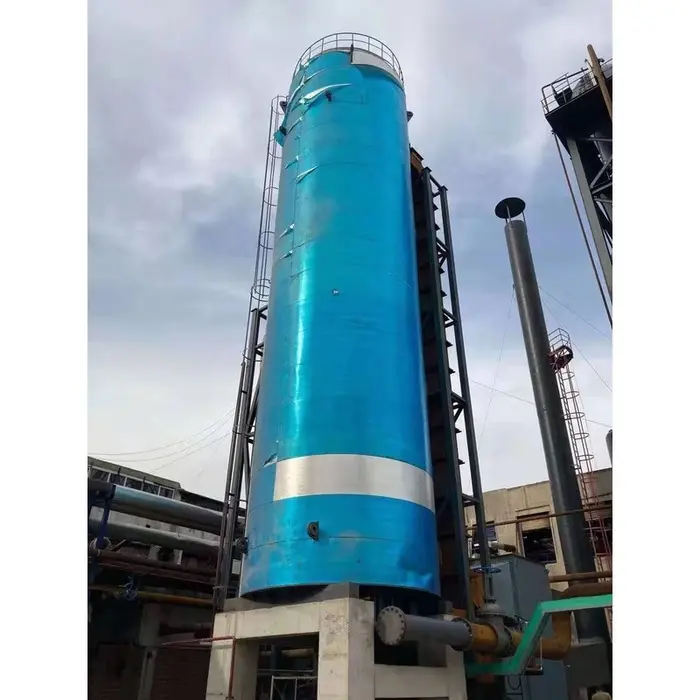
We provide an integrated solution for full-set heating, temperature control and waste heat recovery for asphalt mixing plants, which saves energy and reduces consumption, and ensures stable and compliant asphalt production.