Heating Solution for Chemical Industry
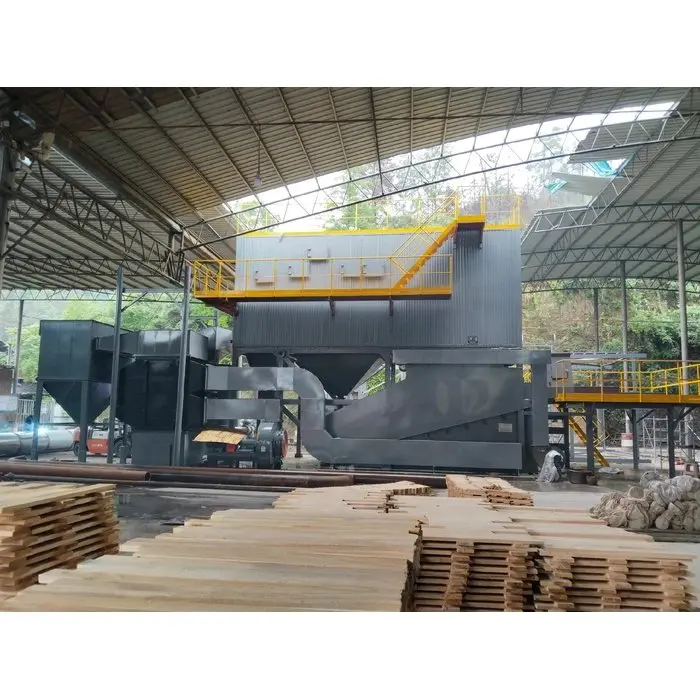
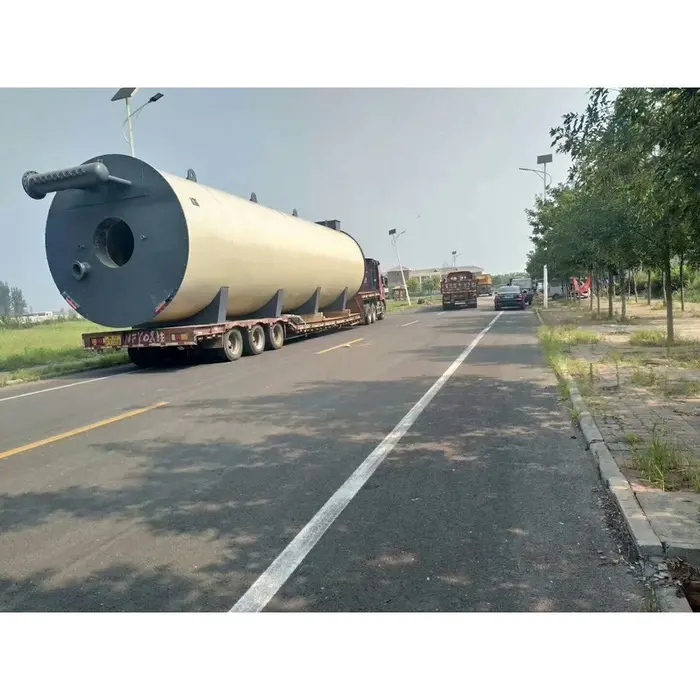
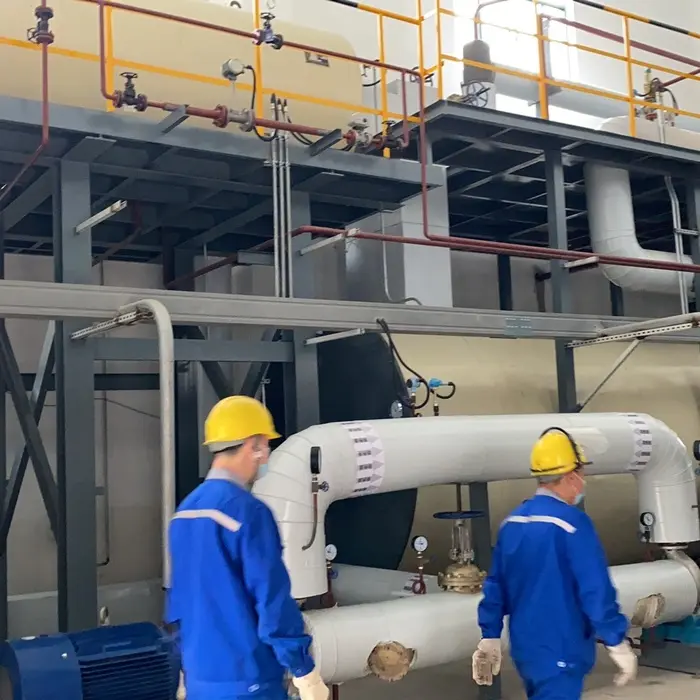
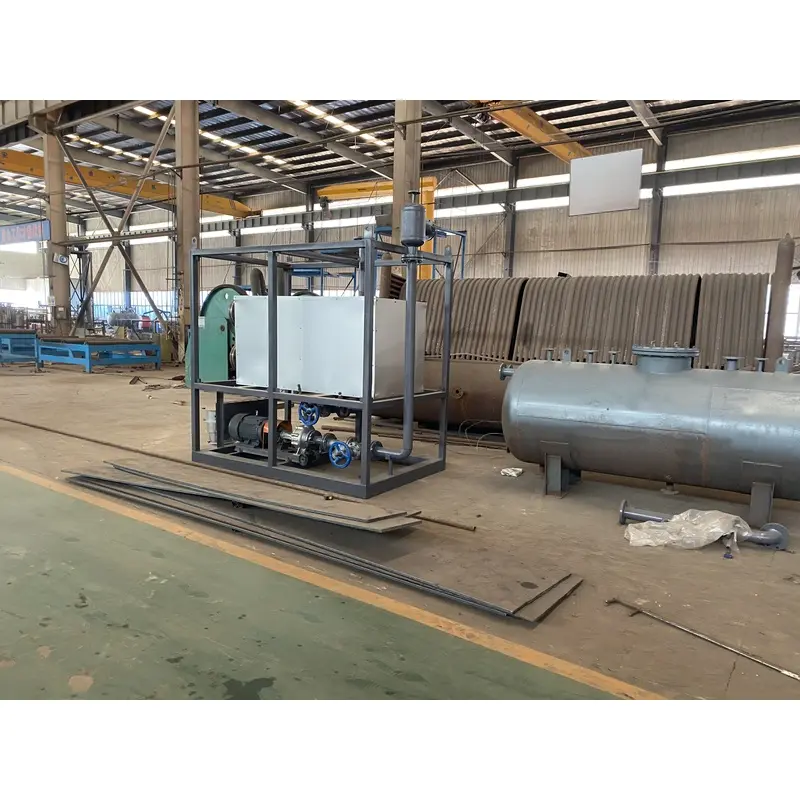
Heating Solution for Chemical Industry Adopts a closed‑loop heating system consisting of "thermal oil heater + high‑temperature circulating pump + heat exchange for heat‑consuming equipment + automatic control". The organic heat‑carrier furnace heats the thermal oil to 280~350℃. Forced circulation by the high‑temperature circulating pump delivers hot oil stably to heat‑consuming equipment such as reaction kettles, distillation columns and evaporators to achieve precise constant‑temperature heating. It features high temperature‑control accuracy, safe and reliable operation under atmospheric pressure, and thermal efficiency ≥90%. Suitable for heating processes in petrochemicals, fine chemicals, printing & dyeing, oil & fat, asphalt and other industries. Customizable according to heat load, fuel conditions and explosion‑proof grades. Full‑range services including design, supply, installation and operation‑maintenance are available.
1.Overview
This solution delivers a complete high-temperature thermal oil (heat transfer fluid) heating system for the petrochemical, fine chemical and pharmaceutical industries. Thermal oil is heated to 280–350°C in an organic heat carrier (thermal oil) boiler and circulated by high-temperature pumps in a closed loop, providing stable, precise heat to reactors, distillation columns, evaporators and other process equipment.
2.Technical Route
Closed-loop heating architecture: thermal oil boiler + circulation system + heat-exchange units + automatic control.
Heat source: organic heat carrier boiler fired by gas / oil / electricity / waste-heat recovery; outlet oil temperature up to 350°C;
Circulation: high-temperature pumps force closed-loop circulation; heat absorbed in the boiler is released at the user end, and the cooled oil returns for reheating; system thermal efficiency ≥ 90%;
Control: PLC/DCS automatic temperature control precisely regulates outlet temperature and flow (accuracy ±1~2°C);
Safety: expansion tank, storage tank, high/low level, differential-pressure and over-temperature alarms, plus emergency shutdown interlock.
3.System Components
Organic heat carrier (thermal oil) boiler, high-temperature circulation pump sets and piping, expansion tank, storage tank, oil charging/filtration system, heat-exchange units (reactor jackets, distillation reboilers, etc.), instrumentation and automatic control system.
4.Key Advantages
High temperature at low pressure: up to 300°C+ heating under atmospheric pressure, no high-pressure vessel risk;
Precise temperature control: minimal fluctuation, meeting strict constant-temperature requirements of fine chemicals;
High efficiency & energy saving: high thermal efficiency, further savings with flue-gas waste-heat recovery;
Reliable & low maintenance: closed-loop design extends thermal oil service life;
Safe & eco-friendly: multiple interlocks, fully sealed operation, no leakage.
5.Applications
Petrochemical: reactor heating, distillation, rectification, dehydrogenation;
Fine chemical: dyes, pigments, pharmaceutical intermediates, resin constant-temperature reactions;
Others: textile setting, oil & fat processing, asphalt heating, coating curing.
6.Customization & Service
Non-standard design according to heat load, temperature requirement, fuel type (natural gas /oil/electricity /waste heat) and explosion-proof rating; full-service support from design, equipment supply, installation & commissioning to after-sales maintenance.
Other Solutions
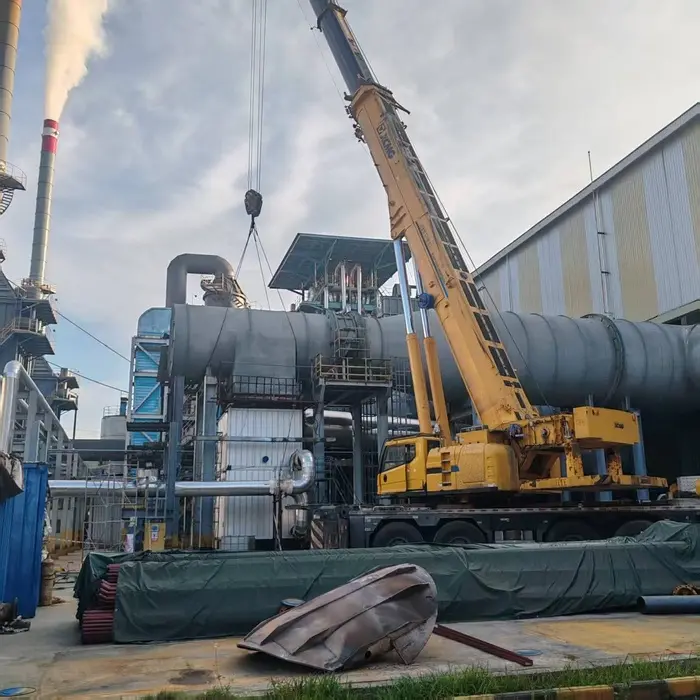
Food Processing Industry Solution
Provide safe and energy‑complete thermal system solutions including thermal oil heaters and waste heat recovery units for heating demands of cooking, drying, sterilization and other processes in food processing, to meet hygienic, stable and compliant production requirements of the food industry.
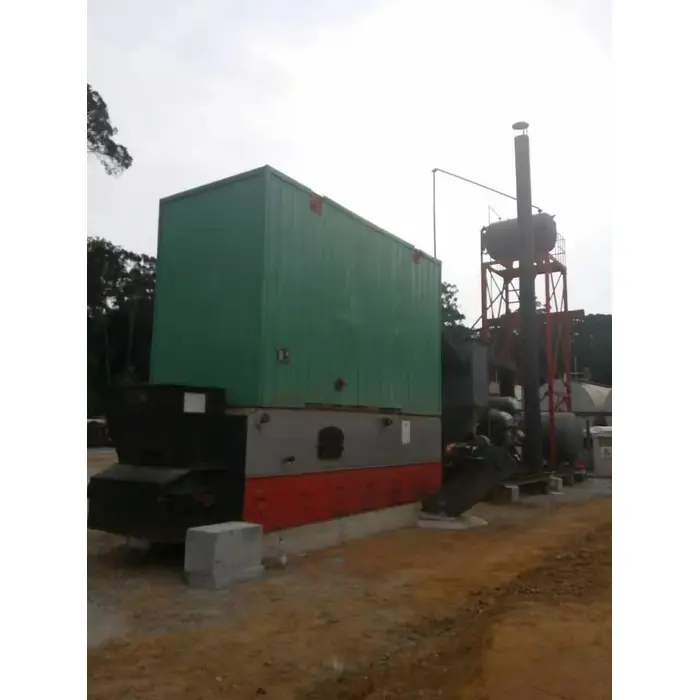
Textile Dyeing Industry Solution
Aiming at the pain points of high energy consumption and high emissions in textile printing and dyeing, we provide an integrated thermal solution of thermal‑oil heater plus waste heat recovery to cut energy consumption in printing and dyeing production, achieving energy‑saving, cost reduction and environmental compliance.
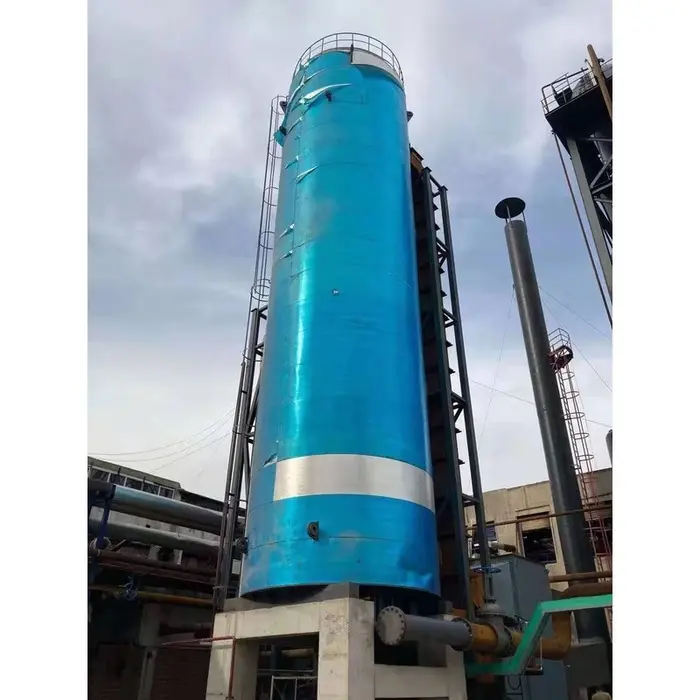
Asphalt Solutions
We provide an integrated solution for full-set heating, temperature control and waste heat recovery for asphalt mixing plants, which saves energy and reduces consumption, and ensures stable and compliant asphalt production.